
Custom molded parts · Made to your design
Custom Injection-Molded Plastic Filter Housings
Define containment and cartridge interfaces before approving the housing.
We review custom filter bodies and closures around their fluid, cartridge and sealing requirements. Share the complete mating geometry so ports, support features and O-ring grooves can be assessed together. Supplying a molded housing does not by itself establish complete filtration performance or a certified pressure rating.
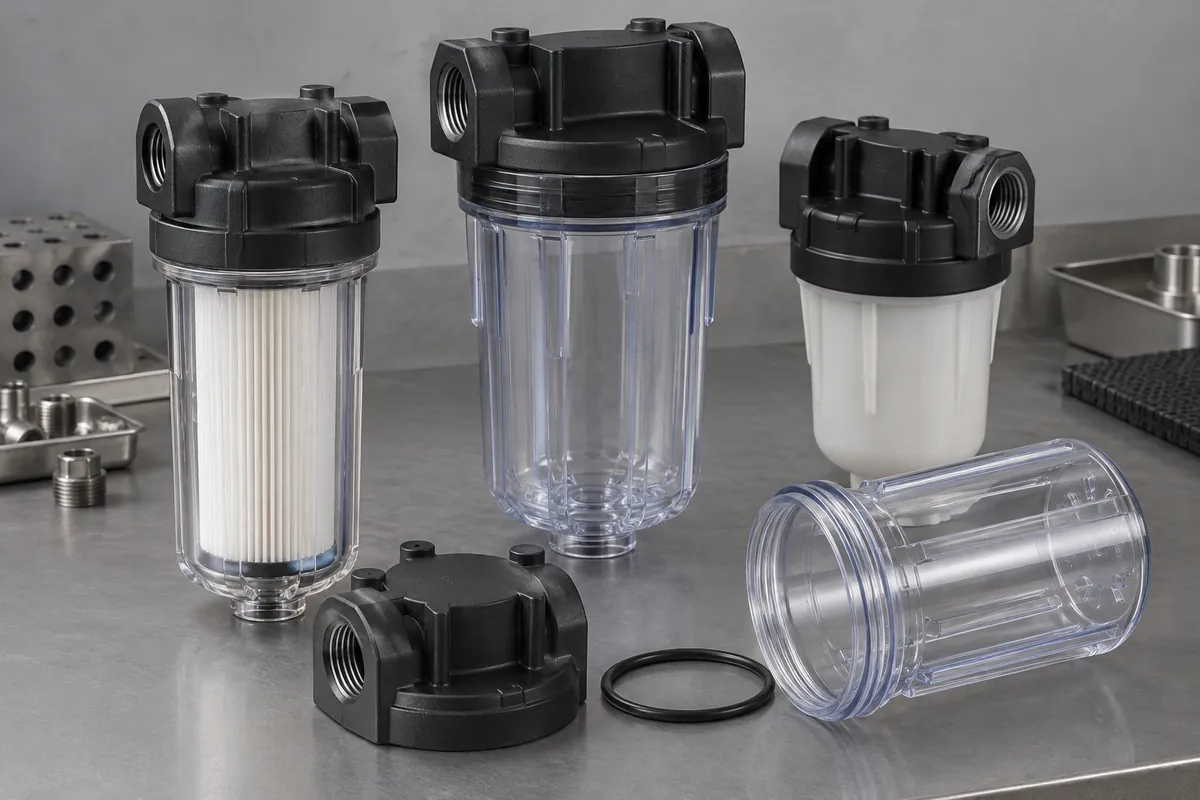
Product details
Plastic Filter Housings: product details
Product design illustrations showing component features and assembly relationships. The final geometry is made to your approved drawing.
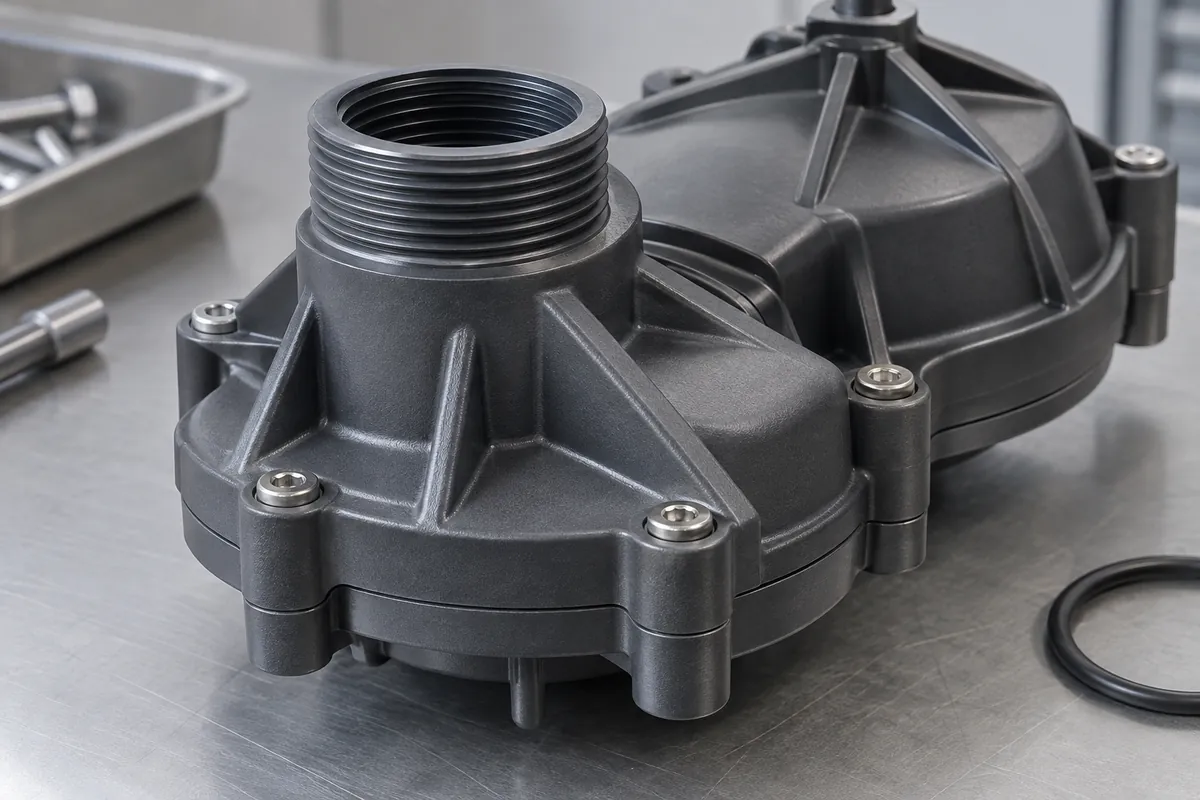
Fluid port
Review thread form and local support around the connection.
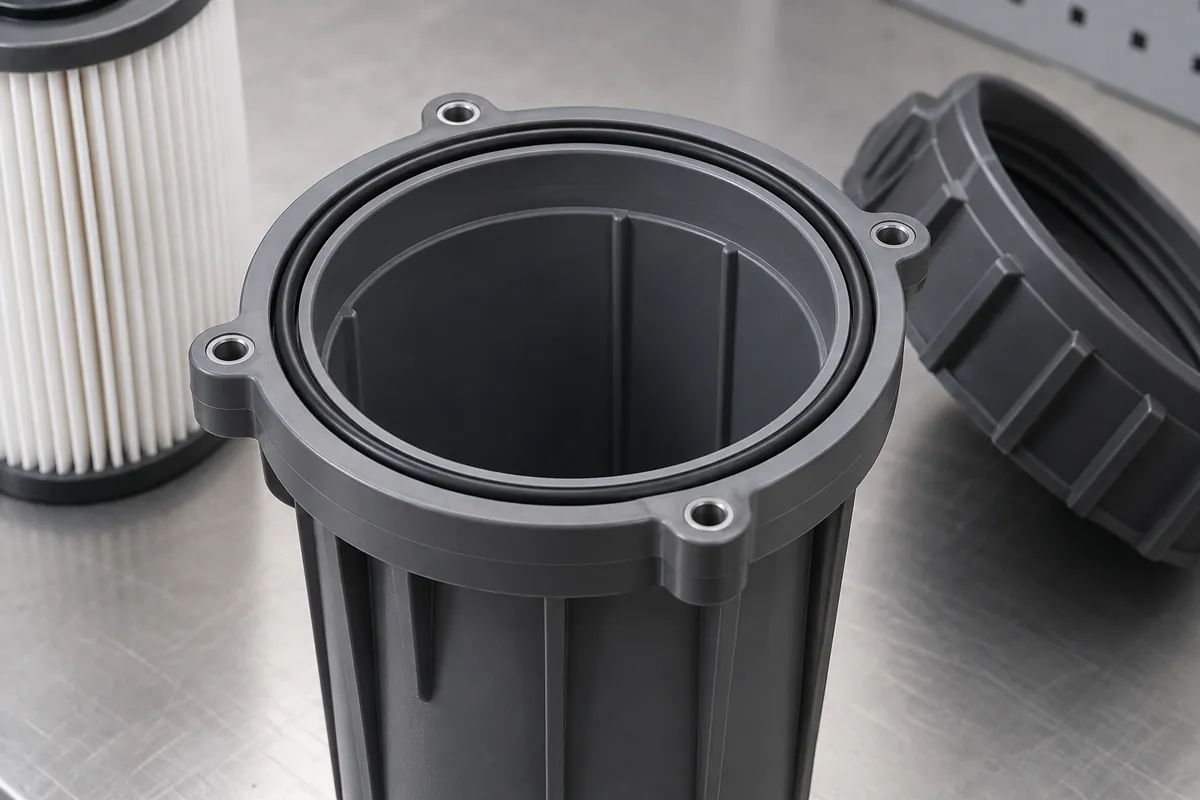
Seal groove
Match the groove, seal and mating component tolerance stack.
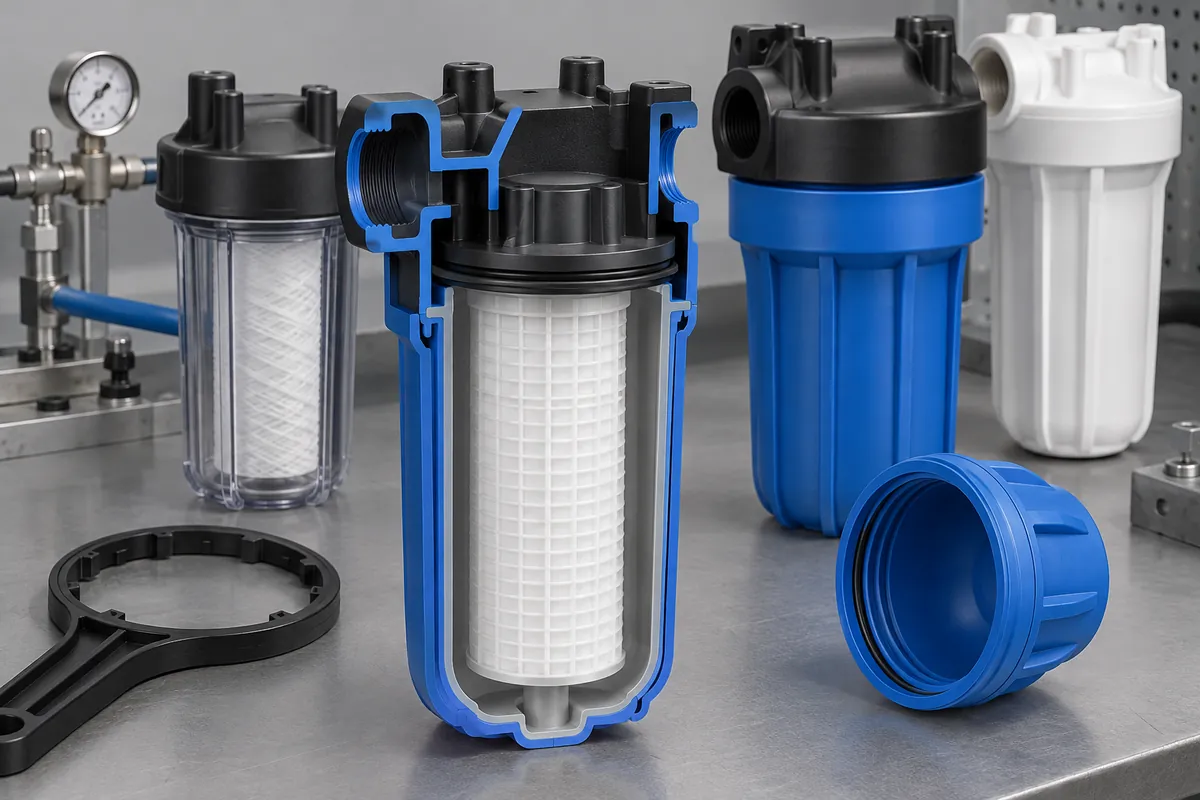
Housing wall
Assess wall transitions against loading and molding.
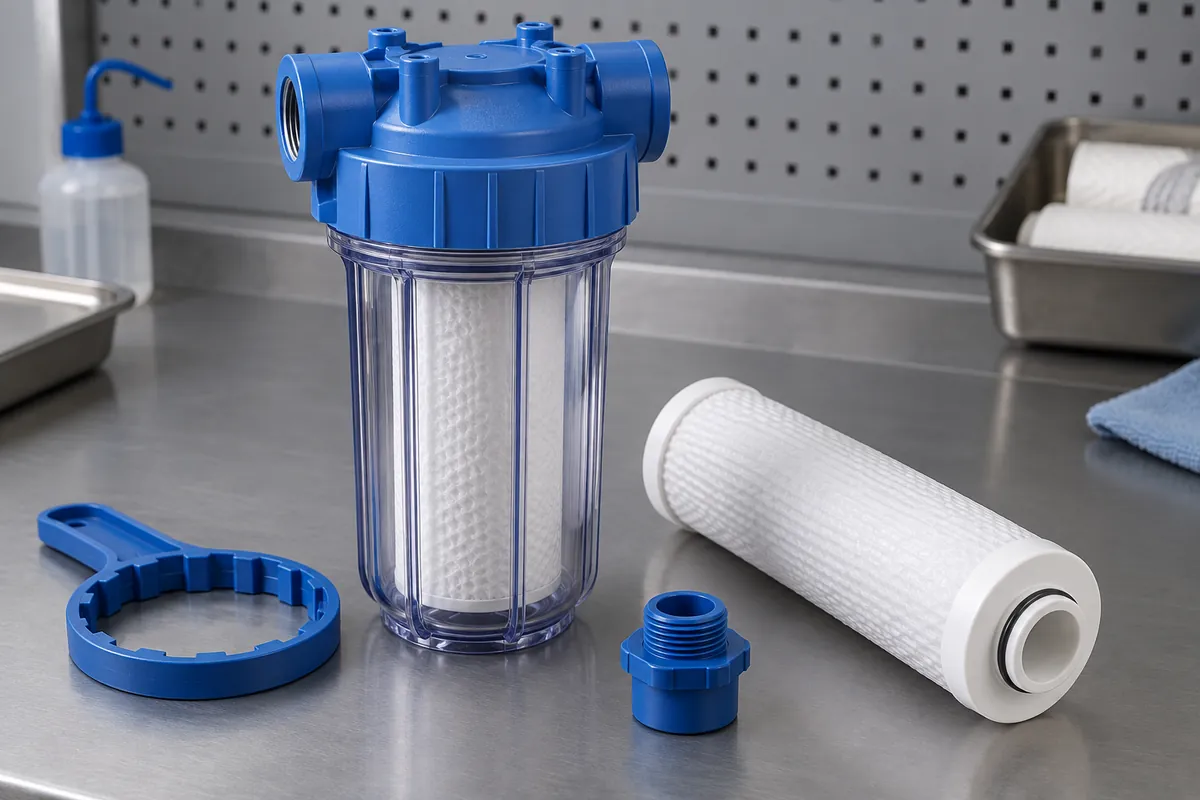
Cartridge seat
Keep clean-side and dirty-side interfaces defined.
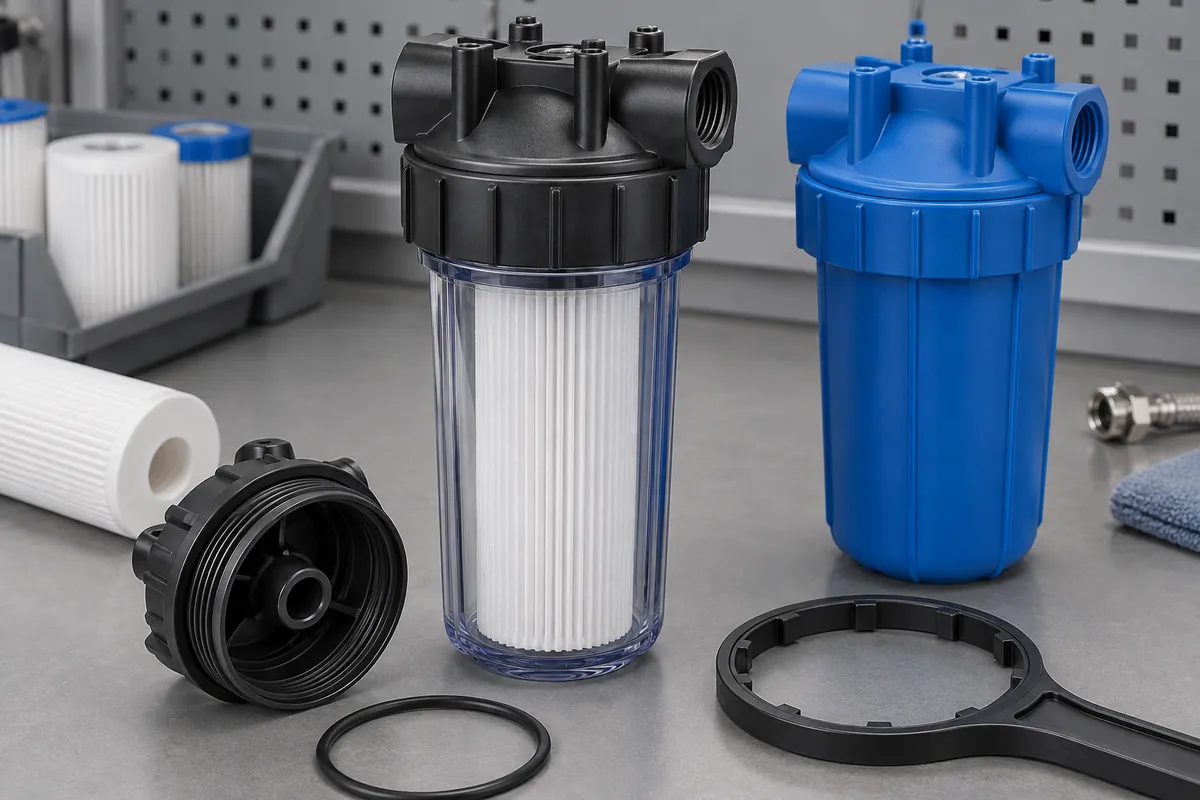
Closure alignment
Specify the finished joining or serviceable closure configuration.
Illustrative configurations. Final specifications follow your approved drawings.
Application fit
A custom component with a defined purpose
Define containment and cartridge interfaces before approving the housing.
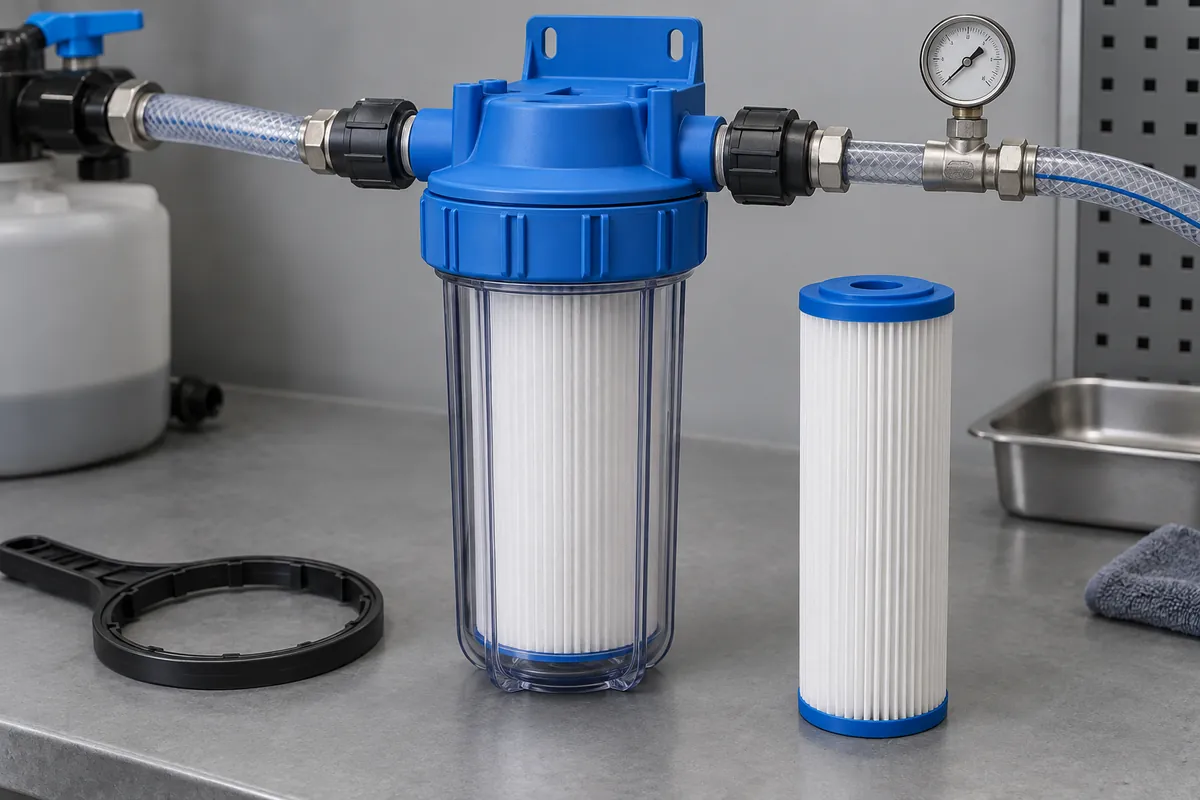
Bodies and bowls
Fluid-contact housings with defined walls, base transitions and port geometry.
Caps and closures
Threaded or joined constructions reviewed against service access and sealing needs.
Cartridge interfaces
Seats, spigots and support features controlling installation and internal flow separation.
Quote-ready inputs
What to send for a meaningful quotation
Use the same drawing and requirements for every proposal. Mark open decisions explicitly so that a low price does not conceal a different deliverable.
| Area | Please provide | Review before release |
|---|---|---|
| Project definition | Current CAD, drawing revision, mating components and quantities. | Mark fixed interfaces and open design decisions before comparing quotations. |
| Fluid duty | Fluid composition, cleaning, temperature and pressure profile. | Screen exact grades and all contacting seals. |
| Interfaces | Cartridge revision, O-ring, thread form and closure method. | Separate retention, external sealing and internal bypass control. |
| Acceptance | Leak, proof, burst and endurance methods where required. | Do not convert an unfinished pressure test into a service rating. |
| Supply and release | Trial, first-order and repeat quantities, packing and report needs. | Agree tooling scope, approval hold points and change control. |
From drawing to approval
From the assembly requirement to production approval
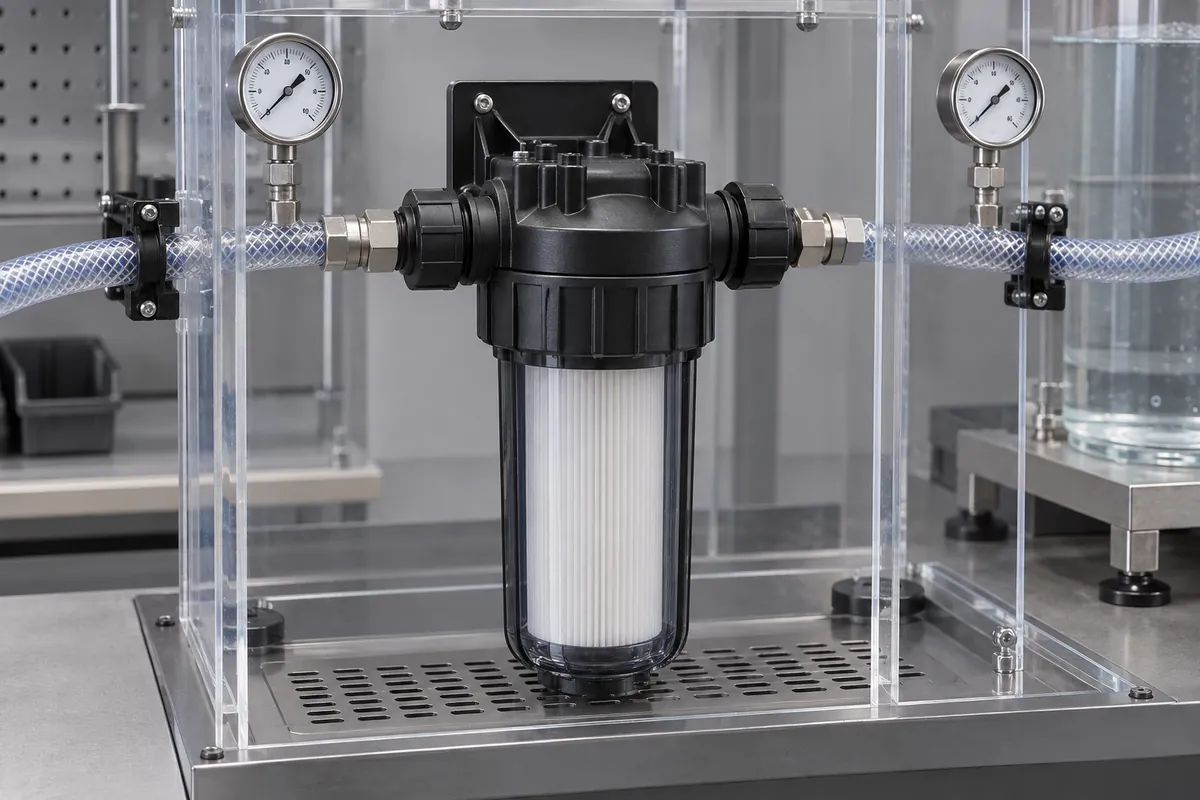
Align the scope
Define the fluid boundary, review molding and closure geometry, evaluate identified samples, then complete the agreed dimensional and assembly tests.
Review the tool and material
Confirm the exact compound, molding route and any secondary operations. Resolve proposed changes against the functional drawing before tooling release.
Evaluate identified samples
Record cavity and lot identity with dimensional and agreed functional observations. Keep incomplete validation separate from completed acceptance.
Release the approved configuration
Retain the drawing, material, process route and inspection method. Review later changes against the configuration that was actually approved.
Practical engineering and buying guides
Decisions to make before production
- Plastic Filter Housing Materials: PP, PA or PVDF?Compare PP, PA and PVDF for molded filter housings using the actual fluid, temperature, pressure cycle and sealing interfaces. Keep resin data separate from assembly ratings.
- Threaded vs Welded Plastic Filter HousingsCompare threaded and welded plastic filter housings through service access, sealing, joining control and complete assembly validation. Define the delivered configuration.
- O-Ring Grooves in Molded Filter Housings: Dimensions and CreepReview molded filter-housing O-ring grooves through seal size, gland geometry, surface condition, tolerances and assembly. Avoid universal squeeze values without an application.
- Leak, Proof and Burst Tests for Plastic Filter HousingsDistinguish filter-housing leak, proof-pressure and burst tests. Define medium, temperature, assembly, duration and sample scope without turning a short test into a service rating.
- Molding Threads in Filter Housings: Tooling OptionsDesign molded filter-housing threads with a defined thread form, sealing mechanism, tooling route, engagement and gauge plan. Review internal and external threads separately.
- Filter Cartridge-to-Housing Fit: Seals, Stops and Bypass PathsReview filter cartridge fit, end seals and internal bypass paths separately from external housing leakage. Define tolerance stacks, support and complete filtration validation.
Before you request a quote
Does a housing leak test verify filtration efficiency?
No. Internal bypass and media performance need separate evaluation in the complete filter.
Can the part be advertised as FDA approved because of the resin?
No. Any contact claim must match the exact material, processing and intended use documentation; it is not a generic housing approval.
Can internal ports be molded directly?
That depends on thread geometry, tooling and material. Confirm the release method and appropriate gauge plan during DFM.
Your next step
Discuss the part with its intended function.
Send the plastic filter housings drawing with its mating interfaces and acceptance requirements. We will review the proposed molding scope and identify the information needed for a meaningful quotation.
Explore our injection molding service or review other custom molded applications.